Training where the work happens — not in a classroom far from the machineTraining वहीं जहाँ काम होता है — मशीन से दूर classroom में नहीं
For MSMEs in manufacturing, quality is often treated as an end-of-line inspection problem. A batch fails, warranty claims rise, and the floor scrambles to reject defective units. But true manufacturing quality is not inspected into a product — it is trained into the workforce.Manufacturing MSMEs के लिए quality अक्सर end-of-line inspection की समस्या बन जाती है। Batch fail, warranty claims बढ़े, और floor defective units reject करने दौड़ पड़ता है। असली manufacturing quality product में inspect नहीं की जाती — workforce में train की जाती है।
Drawing from Su-Kam's structured battery plant training blueprint, here is how to institutionalize shop-floor education, monitor critical machine parameters, and eliminate defects at the source. Companion to engineering warranty out of the battery line: training is how that engineering reaches every shift.Su-Kam के structured battery plant training blueprint से: shop-floor education कैसे संस्थागत करें, critical machine parameters कैसे monitor करें, और source पर defects कैसे खत्म करें। battery line से warranty बाहर निकालने का साथी: training वह रास्ता है जिससे engineering हर shift तक पहुँचती है।
The Six Pillars of Plant TrainingPlant Training के छह स्तंभ
A structured curriculum must cover every critical touchpoint — not informal tribal knowledge. Our battery plant framework broke operations into six areas:Structured curriculum हर critical touchpoint को cover करे — informal tribal knowledge नहीं। हमारे battery plant framework ने operations को छह क्षेत्रों में बाँटा:
- Grid Casting: Defect awareness, probable causes, and tracking weight and thickness.
- PDC (Pressure Die Casting): Critical machine and product parameters during PDC and spine cutting.
- Assembly: SOPs and strict work instructions.
- Acid Filling: Precise volumetric handling and defect prevention.
- Charging: In-process check sheets for electrical and thermal parameters.
- HRD (High Rate Discharge): Final validation and testing protocols.
- Grid Casting: Defect awareness, probable causes, और weight व thickness ट्रैक करना।
- PDC (Pressure Die Casting): PDC और spine cutting के दौरान critical machine और product parameters।
- Assembly: SOPs और सख्त work instructions।
- Acid Filling: सटीक volumetric handling और defect prevention।
- Charging: Electrical और thermal parameters के लिए in-process check sheets।
- HRD (High Rate Discharge): Final validation और testing protocols।
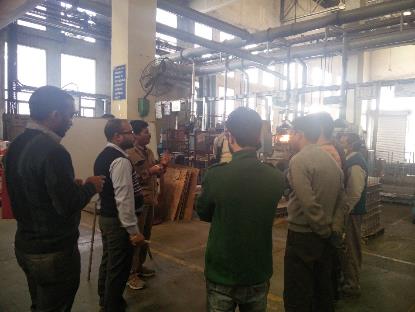
Grid casting session — defect awareness beside the lineGrid casting session — line के बगल में defect awareness
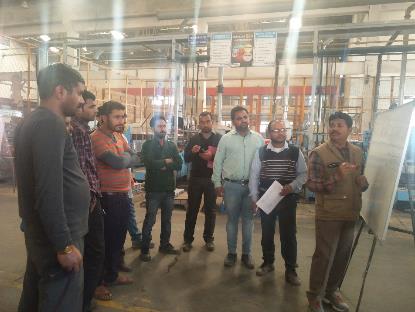
Whiteboard + check sheet in hand — the session is incomplete without bothWhiteboard + हाथ में check sheet — दोनों के बिना session अधूरा
From Informal Control to Statistical Limitsअनौपचारिक नियंत्रण से Statistical Limits तक
One of the greatest MSME gaps is the absence of statistical process control on the floor. Operators run machines by intuition instead of hard limits.MSMEs की सबसे बड़ी gaps में से एक — floor पर statistical process control का अभाव। Operators intuition से मशीन चलाते हैं, hard limits से नहीं।
- Control limits beside the machine: Teach workers to map Upper Control Limit (UCL), Mean, and Lower Control Limit (LCL) on a whiteboard at the station. When a parameter drifts outside those lines, the operator must know a defect — flash, short run, crack, shrinkage — is imminent.
- In-process check sheets: Daily filling is mandatory. That creates accountability and an auditable trail for plant managers.
- मशीन के बगल में control limits: Workers को station पर whiteboard पर UCL, Mean, और LCL मैप करना सिखाओ। जब parameter उन रेखाओं से बाहर जाए, operator को पता होना चाहिए — flash, short run, crack, shrinkage — defect आने वाला है।
- In-process check sheets: रोज़ भरना अनिवार्य। इससे accountability और plant managers के लिए auditable trail बनती है।
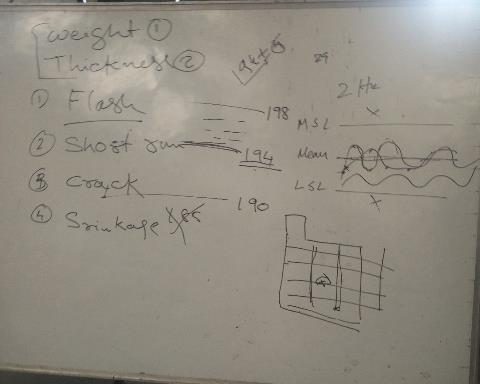
Live board from grid casting training — weight, thickness, defect names, and control linesGrid casting training का live board — weight, thickness, defect names, और control lines
Acid Filling and Process RigorAcid Filling और Process Rigor
In battery production, small execution errors become catastrophic field failures.Battery production में छोटी execution गलतियाँ field में बड़ी failures बन जाती हैं।
- Defect awareness: Acid filling and charging sessions focus on root causes of process variation before they shorten battery life.
- Standardized work instructions: Every operator learns precise dos and don'ts so human error is engineered out of the line — same discipline as protection engineered into the product.
- Defect awareness: Acid filling और charging sessions process variation के root causes पर ध्यान देते हैं — battery life घटने से पहले।
- Standardized work instructions: हर operator सटीक dos और don'ts सीखे ताकि human error line से बाहर हो — वही अनुशासन जो product में protection engineering में था।
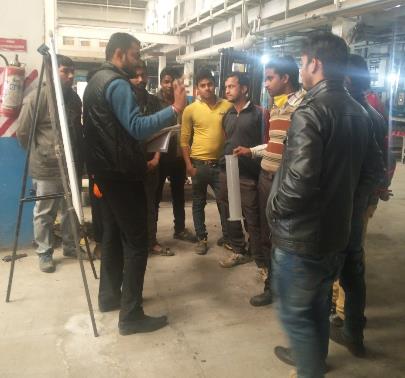
Acid filling & charging — volumetric rigor with the cylinder in the circleAcid filling & charging — circle में cylinder के साथ volumetric rigor
The Core Message for MSME FoundersMSME Founders के लिए मूल संदेश
Your factory is only as good as the operator standing at the machine. Train your people to understand the why behind every parameter, and quality will take care of itself.तुम्हारी फैक्ट्री केवल उस operator जितनी अच्छी है जो मशीन पर खड़ा है। लोगों को हर parameter के पीछे का why समझाओ — quality खुद संभल जाएगी।
Structured shop-floor training is not overhead — it is the competitive advantage. When the workforce owns control limits, defect root causes, and SOP compliance, you cut waste, slash warranty returns, and build a plant that stays world-class across shifts.Structured shop-floor training overhead नहीं — competitive advantage है। जब workforce control limits, defect root causes, और SOP compliance अपना लेती है, waste कटता है, warranty returns गिरते हैं, और हर shift पर world-class plant बनता है।
The 5 Training Rules for Hardware MSMEsHardware MSMEs के लिए Training के 5 नियम
- Train at the machine, not only in a hall: Context is half the lesson.
- Cover every critical process as a pillar: Casting through final test — no orphan stations.
- Put UCL / Mean / LCL on a board operators can see: Intuition is not a control plan.
- Make check sheets non-negotiable: No sheet, no run.
- Teach the why of every dos and don'ts: Compliance without understanding dies on the night shift.
- सिर्फ hall में नहीं — मशीन पर train करो: Context आधा पाठ है।
- हर critical process को pillar बनाओ: Casting से final test तक — कोई orphan station नहीं।
- UCL / Mean / LCL board पर लगाओ जिसे operator देखे: Intuition control plan नहीं।
- Check sheets गैर-परक्राम्य बनाओ: Sheet नहीं, run नहीं।
- हर dos और don'ts का why सिखाओ: बिना समझ की compliance night shift पर मर जाती है।